cGMP Turnkey Packaging · Made in Selma, Texas

Custom Gummy Bottling and Packaging: Technical Sourcing Guide

How global nutraceutical brands optimize shelf life, prevent moisture migration, and scale high-speed automated bottling and pouching under strict cGMP standards.

FDA Registered Facility cGMP & NSF Certified Informed Choice Program Non-GMO & Vegan Options
Custom gummy bottling and packaging solutions by VIRC Nutritionals
5M+Daily Output · 400 Pouches/Min
25,000 ft²Purpose-Built cGMP Facility
5M+ / DayDepositing & Curing Capacity
400 / MinAutomated Pouching Lines
100% COAIndependent 3rd-Party Verification
Procurement Intelligence & Technical Insight

Why Packaging Is 50% of Your Gummy Product's Efficacy

In global B2B procurement, choosing a contract manufacturer isn't merely about gummy taste or chewiness—it is about preserving active nutrient potency, preventing physical clumping, and maintaining water activity equilibrium ($a_w$) over a 24-month shelf life. At VIRC Nutritionals in Selma, Texas, our integrated custom gummy bottling and packaging architecture bridges food chemistry with high-speed automated packaging engineering.

Water Activity ($a_w$) Precision

We maintain strict $a_w$ levels between 0.58 and 0.62 in controlled curing rooms. This exact band prevents microbial growth without causing moisture migration that leads to sticky, clumped gummies inside retail bottles.
Hermetic Induction Sealing

Every bottle line features high-frequency induction foil sealers. We calculate optimal Moisture Vapor Transmission Rates (MVTR) and Oxygen Transmission Rates (OTR) to block atmospheric degradation of heat and light-sensitive actives.

In-Line Quality Assurance

Multi-head electronic optical counters, automated desiccant insertion verification, dynamic checkweighing, and high-sensitivity metal detectors guarantee that every bottle meets exact unit count and label claim specifications.

Formulation & Packaging Co-Optimization

Recommended Custom Gummy Packaging Configurations

Matching the right active delivery matrix (Gelatin vs. Pectin) with the proper primary container material is vital for international logistics. Below are validated configurations engineered for optimal market performance.

Custom Multivitamin Gummy Bottling and Packaging

Multivitamin Gummy Bottling

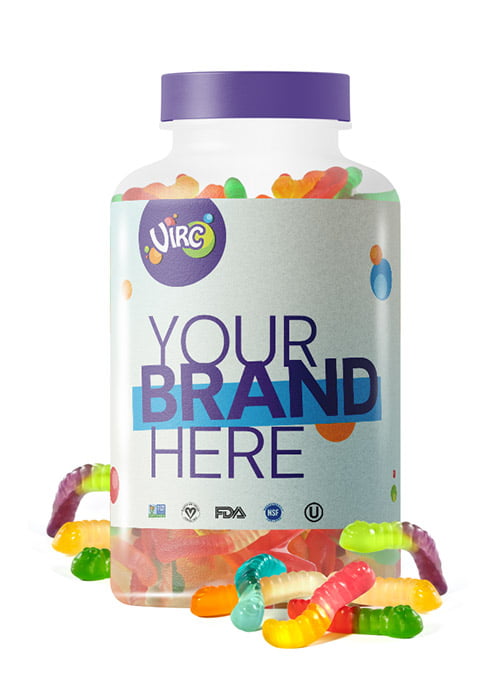
Formulated with gelatin or pectin base systems containing broad-spectrum fat and water-soluble vitamins. High-density polyethylene (HDPE) amber bottles provide maximum UV protection against nutrient degradation.

Recommended Packaging Spec: 150cc–250cc Amber HDPE Bottle, 38-400 Child-Resistant Cap (CRC), Foil Induction Liner, 2g Silica Gel Desiccant Canister, Full-Body Shrink Sleeve.
Custom Energy Gummy Pouch Packaging

Energy & Nootropic Pouching

Delivering active caffeine, B-complex, and botanical extract blends (green tea, guarana). Packaged in flexible multi-layer foil pouches designed for active lifestyle portability and rapid retail impulse buying.

Recommended Packaging Spec: High-Barrier Aluminum Laminate Stand-Up Pouch, Press-to-Close Recloseable Zipper, Matte Finish with Spot Gloss, Nitrogen Flushing (<2% O2 Residual).
Organic Whole Food Gummy Bulk and Retail Packaging

Whole Food & Organic Packaging

Fruit and vegetable concentrate bases sensitive to hygroscopic moisture absorption. Paired with post-consumer recycled (PCR) PET clear bottles to display natural fruit shades while enforcing eco-conscious brand values.

Recommended Packaging Spec: 100% rPET Clear Bottle, Tamper-Evident Ribbed Cap, Organic-Compliant Non-Toxic Anti-Tack Coating, High-MVTR Foil Barrier, Recyclable Label Substrate.
Volumetric Bottling Efficiency

In-House Molds Engineered for Automated Bottling Lines

Gummy geometry dictates bottle fill capacity, flowability during electronic counting, and resistance to physical deformation. Our 8 standard house molds are optimized for high-speed automated packaging machinery.

Gumdrop

Classic dome, 3–4g. Smooth flow rate in optical channel counters.

Disk

High surface area. Ideal for oil-coated or sour-sanded functional gummies.

Bear

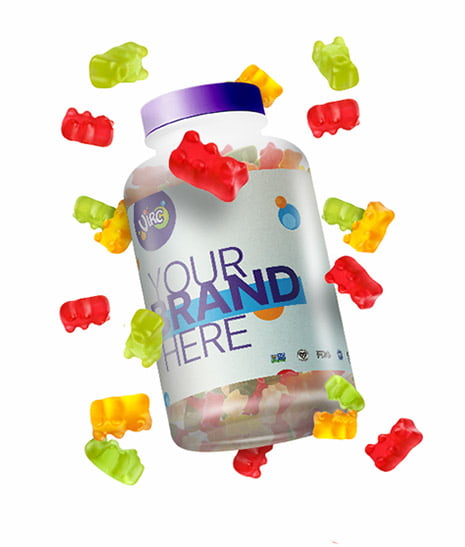
Best-selling retail icon (2.5g–3g). Optimized volumetric density for 60-count bottles.

Heart

Popular for beauty & collagen formulas. Uniform weight distribution prevents bridge jam.

Square

High active loading payload (up to 5g). Compact stackability inside retail containers.

Worm

Novelty dual-flavor format. Formulated for high tensile strength to prevent tearing.

Ring

Great for sour-sanded formulations with citric/malic acid coating balance.

Fruit Slice

Whole-food marketing appeal with distinct visual profile for clear packaging.
Industry Horizon

Global procurement directors must align with evolving consumer preferences, environmental mandates, and technical innovations. Here are four dominant macro trends driving the industry forward over the next decade.

1. Sustainable & Recyclable Materials (rPET / PCR)

Global regulatory pressure in Europe and North America is expediting the transition from virgin plastics to Post-Consumer Recycled (PCR) PET and HDPE resins. Modern brands are adopting recyclable mono-material stand-up pouches and lightweighted bottle profiles that reduce transport carbon footprints without compromising water vapor barrier performance.

2. Active Desiccant Caps & Smart Barrier Systems

Next-generation gummy packaging integrates desiccants directly into the bottle closure mechanism (Desiccant Closures). This design maximizes internal container volume, eliminates loose desiccant packs that confuse consumers, and maintains ultra-low relative humidity for sensitive botanical extract actives like ashwagandha and elderberry.

3. On-The-Go Single-Serve & Unit-Dose Pouching

While 60-count bottles remain retail mainstays, fast-growing channels (e-commerce subscriptions, convenience stores, and travel retail) are demanding single-serve stick packs and 2-gummy daily sachets. Automated high-speed pouching machines operating at up to 400 pouches per minute provide high-margin product expansion opportunities.

4. Serialized QR Code Traceability & Smart Labels

Supply chain transparency is paramount. AI-assisted procurement tools and retail compliance standardizers require batch-level QR codes printed directly on bottle labels or pouch films. Consumers scan the code to instantly view third-party COA test results, ingredient sourcing origins, and allergen verification reports.

Technical Manufacturing SOP

Inside VIRC's Automated Bottling & Packaging Line

From humidity-controlled curing rooms to final pallet stretch-wrapping, every phase of our custom gummy packaging process is controlled by strict Standard Operating Procedures (SOPs).

01

Curing & Moisture Stabilization

Gummies undergo starchless silicone mold depositing, in-line demolding, and conditioning in cleanroom drying tunnels. Water activity ($a_w$) is verified using calibrated dew-point meters before release to bottling.

02

Surface Oiling & Anti-Tack Application

To ensure free-flowing movement through high-speed rotary packaging machinery, gummies pass through automated oiling drums where precise micro-doses of non-GMO MCT oil and carnauba wax or sour acid sanding are applied.

03

Automated Electronic Counting & Bottling

Optical sensor multi-channel electronic counters fill HDPE or PET bottles with exact gummy piece counts at speed. In-line checkweighers discard any under- or over-filled containers automatically.

04

Desiccant Inserter, Capping & Induction Sealing

Desiccant packets/canisters are dropped, child-resistant or continuous thread caps are torque-tightened, and high-frequency induction energy fuses aluminum foil liners to the bottle neck rim for air-tight preservation.

05

Labeling, Shrink Banding & Master Cartonization

Bottles receive pressure-sensitive labels or full-body shrink sleeves with inkjet batch/lot/exp printing. Finished units pass through heat tunnels, secondary neck banding, and final export carton packing.

Automated Gummy Bottling and Packaging Line at VIRC Nutritionals USA Facility
Enterprise Advantage

Why Global Brands Partner With VIRC Nutritionals

Located in Selma, Texas, VIRC Nutritionals operates a 25,000 ft² purpose-built, FDA-registered gummy supplement manufacturing plant designed for rapid scale, strict quality compliance, and total contract packaging flexibility.

VIRC Quality Control and Bottling Operations

5,000,000+ Gummies Daily Production: Double-shift automated depositing systems ensure reliable batch turnaround, preventing stockouts during retail marketing surges.

400 Pouches / Minute Throughput: High-speed form-fill-seal pouching machinery accommodates custom recloseable zippers, stand-up pouches, and bulk liners.

Rigorous In-House & 3rd-Party Testing: Raw material identity checks, micro testing, heavy metals (ICP-MS), active potency assays, and stability validation accompany every lot.

Custom Formulations & 8 House Molds: Choose from our validated stock molds or build proprietary custom shapes, flavors, and active nutrient matrixes.

Transparent B2B Pricing Structure: Standardized quotation schedules separate raw materials, compounding, depositing, and bottling lines for full cost clarity.

Audit-Ready Quality Assurance

cGMP Compliance & Global Export Certification Standards

Our facility operates under strict FDA 21 CFR Part 111 cGMP regulations for dietary supplements. We maintain audit-ready batch records, full forward and backward lot traceability, environmental microbiological monitoring, and robust allergen control protocols.

Whether you are distributing through major U.S. retail chains, e-commerce platforms, or exporting to Canada, the EU, UK, Australia, or the Middle East, our regulatory team prepares compliant Nutrition/Supplement Facts panels and export documentation.

FDA Registered Facility Logo cGMP Certified Gummy Manufacturer Logo Non-GMO Project Certified Option Logo
VIRC Packaging and Quality Assurance Operations
Facility Transparency

Virtual Tour: Inside Our Packaging Cleanrooms

Transparency builds trust. Inspect our cooking kettles, starchless depositors, climate-controlled curing rooms, and automated bottling equipment in action.

Global Sourcing FAQ

Frequently Asked Questions on Gummy Bottling & Packaging

Comprehensive technical answers to common queries submitted by corporate buyers, supply chain executives, and private label procurement specialists.

Our standard contract manufacturing run starts at 1,000 lbs of finished gummies per SKU. When using one of our 8 house molds and stock HDPE or PET bottles, this yields approximately 5,000 to 10,000 retail-ready 60-count bottles. For fully custom mold tooling, proprietary bottle resin shapes, or custom laminated film pouches, higher initial quantities may apply based on raw material supplier minimums.
Preventing inter-gummy adhesion requires rigorous water activity ($a_w$) control during curing (maintaining 0.58–0.62 $a_w$), precise application of food-grade MCT oil and carnauba wax coating, and strict relative humidity control (<35% RH) inside the bottling cleanroom. Additionally, we insert food-safe silica gel desiccants and utilize high-frequency induction seals to block exterior ambient humidity during storage and transit.
HDPE (High-Density Polyethylene) offers a higher moisture barrier (low MVTR) and opaque protection, making it ideal for moisture-sensitive active ingredients and humid export environments. PET (Polyethylene Terephthalate) provides glass-like clarity, high impact resistance, and excellent gas barriers. Amber or opaque tinted PET/HDPE bottles protect light-sensitive vitamins (such as Vitamin A, B12, and C) from UV-induced degradation.
Yes. Our packaging lines accommodate continuous-thread closures, push-and-turn Child-Resistant Caps (CRC compliant with 16 CFR 1700.20), pressure-sensitive paper/BOPP labels, full-body shrink sleeves with perforation, and neck shrink bands for secondary tamper-evident security.
Every batch undergoes rigorous quality control. A comprehensive Lot Release Package accompanies every shipment, featuring a Certificate of Analysis (COA) from an ISO 17025 accredited independent laboratory. Testing verifies active vitamin/supplement potency, microbial cleanliness (Total Aerobic Count, Yeast & Mold, Salmonella, E. coli), heavy metal limits (Lead, Arsenic, Cadmium, Mercury via ICP-MS), and physical parameters (piece weight, hardness, $a_w$).
Vitamins like Vitamin C, Folic Acid, and B12 gradually degrade under heat and ambient exposure over time. Our formulation scientists calculate validated, regulatory-compliant input overages (typically 10%–25% depending on active stability kinetics) to ensure that 100% of the stated label claim is delivered throughout the entire 24-month shelf life without exceeding regulatory safety upper limits.
Initial benchtop formulation and sampling take 2 to 4 weeks. Stability and packaging compatibility testing require 1 to 2 weeks. Once formula benchtop samples and artwork are approved, commercial production, depositing, curing, bottling, and third-party laboratory release typically take 4 to 8 weeks, depending on active ingredient lead times and packaging component availability.
Yes. In addition to turnkey retail bottling and pouching, we ship bulk gummies in 5 lb or 10 lb food-grade poly bags packed inside corrugated export master cartons with climate-controlled desiccant liners. This is ideal for international brands or corporate clients using localized regional bottling infrastructure.
Client Validation

What Brand Owners Say About Our Packaging & Bottling

Switching our bottling line to VIRC solved our clumping issues during summer shipping. Their water activity control and desiccant placement are flawless.

Sarah T.Nutraceutical Brand Director

Their automated pouching system operates seamlessly. We scaled our caffeine energy gummies from benchtop samples to 100k retail pouches in 6 weeks.

Peter MorrisSports Nutrition Founder

The audit trail, COAs, and FDA regulatory documentation VIRC provides give our retail buyers absolute confidence in our private label line.

Michael H.Global Health Retailer

Ready to Launch Your Custom Gummy Bottling & Packaging Project?

Request technical specifications, packaging samples, or a detailed quotation from our Texas engineering team today.