Select from our validated inventory of high-demand skin health, sport nutrition, teeth whitening, and dietary supplement formulations packaged in CE-compliant bottling and adhesive container formats.
In the modern global nutraceutical ecosystem, international brand owners face an increasingly stringent regulatory landscape. Securing market share across the European Economic Area (EEA), North America, and emerging markets demands more than standard manufacturing—it requires rigorous adherence to CE compliance, cGMP protocols, and precise container-closure engineering.
As premier CE Certified Supplement Bottling Suppliers & Exporters, our facility operates at the intersection of biochemical integrity and automated industrial packaging. Supplement bottling is not merely a container filling process; it is a critical protective barrier that preserves active bio-potency, prevents oxidation, guarantees anti-tampering, and delivers verified label claim compliance across multi-year shelf lives.
For brands exporting dietary supplements, medical nutritionals, or functional cosmetic formulations into European jurisdictions, demonstrating regulatory conformity is non-negotiable. While raw dietary supplements themselves fall under EFSA and national food safety directives, the packaging machinery, bottle materials, induction seals, and cleanroom environmental controls must strictly align with European CE standards (Directive 2006/42/EC on machinery, EC No 1935/2004 for food-contact materials) and cGMP (21 CFR Part 111).
Our integrated production infrastructure eliminates supply chain friction by maintaining dual-compliance frameworks. Every bottling line—from automated multi-head tablet counters to high-torque rotary cappers and induction sealing tunnels—is engineered to meet CE technical dossiers, ensuring seamless customs clearance, zero border detention risk, and complete audit readiness for retail distribution.
Nutraceutical active ingredients, including Creatine Monohydrate, Vitamin C, Hyaluronic Acid, and Nitric Oxide precursor complexes, are highly susceptible to moisture vapor transmission (MVTR) and photo-degradation. Our bottling engineering utilizes pharmaceutical-grade High-Density Polyethylene (HDPE) and Amber Polyethylene Terephthalate (PET) bottles paired with hermetic induction seals.
By applying controlled electromagnetic heat sealing, our automated lines fuse a multi-layer foil-laminate barrier directly to the bottle orifice. This seals out oxygen and moisture, creating a modified atmosphere that sustains 100% ingredient potency from initial capping through international ocean freight transit.
Our 25,000 sq ft Selma, Texas facility consolidates complex manufacturing, active ingredient blending, and automated bottling into one seamless supply chain node.
Equipped with dual-lane electronic multi-channel optical counters and rotary cappers delivering over 400 finished containers per minute with automated desiccant insertion and induction sealing.
Our team of food scientists and formulation chemists engineer gelatin and pectin gummies, solid-dose powders, creams, and liquids with precise active overages to guarantee shelf-life stability.
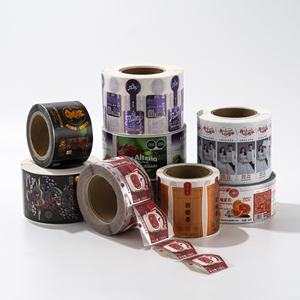
Full-wrap pressure-sensitive adhesive vinyl labels, tamper-evident neck shrink banding, and full-body roll-fed shrink sleeves printed with UV-resistant inks for premium shelf aesthetic.
100% of raw materials and finished lots undergo HPLC, ICP-MS heavy metal, and microbiological testing. A comprehensive Certificate of Analysis accompanies every exported shipment.
Integrating pressure-sensitive neck bands, break-away ring closures, and holographic security seals to meet European retail regulatory guidelines and defeat global counterfeiting.
Seamless international shipping support including custom export tariff coding, multi-lingual outer carton marking, palletized shrink wrapping, and containerized sea/air freight booking.
As consumer demand shifts toward sustainability, transparency, and high-potency functional delivery, procurement executives must align with contract bottling partners who innovate ahead of market dynamics.
Global regulations are rapidly mandating the inclusion of Post-Consumer Recycled (PCR) plastics. Future-ready bottling suppliers are transitioning to 30%–100% rPET and ocean-bound plastics engineered to maintain identical MVTR barrier performance while satisfying EU Directive 2019/904 environmental mandates.
The European Union's digital product passport initiatives are driving a shift from static UPC barcodes to serialized 2D DataMatrix codes. Modern bottling lines print unique lot-specific micro-codes onto bottle bases, enabling consumers and customs officers to scan and instantly verify COA potency, lab reports, and supply chain origin.
Advancements in active packaging incorporate oxygen-scavenging polymers directly into bottle wall linings and cap liners. This technology actively neutralizes trapped headspace oxygen, extending the stability of delicate lipid formulations, probiotics, and natural antioxidant complexes without artificial preservatives.
High-growth nutraceutical brands are abandoning single-SKU manufacturing in favor of agile bottling partners. Modern facilities must offer seamless conversion between traditional HDPE bottle runs, eco-friendly aluminum canisters, and flexible pouch co-packing to capture D2C and omnichannel retail markets.
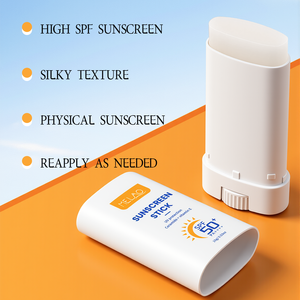
The global dietary supplement market is experiencing a profound paradigm shift. Consumers are increasingly rejecting hard-to-swallow traditional tablets in favor of enhanced sensory experience formats, including pectin nutraceutical gummies, concentrated liquid drops, clear sun sticks, and micro-encapsulated pre-workout powders.
From Creatine Monohydrate muscle-building gummies to multi-strain vitamin complexes, matrix formulation requires precise thermal control during cook and deposit cycles to preserve heat-sensitive actives.
Modern consumers demand non-GMO, vegan, peroxide-free, and allergen-clean formulations. Bottling operations must eliminate cross-contamination risks through automated clean-in-place (CIP) cleanrooms.
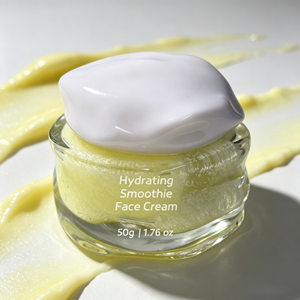
Combining Hyaluronic Acid, Peptide complexes, and Vitamin C into airless pump bottles prevents oxidation, guaranteeing uniform topical delivery and maximizing anti-aging brightening efficacy.
We combine U.S. manufacturing quality and cGMP rigor with competitive global export pricing, offering brand owners a single accountable partner from raw formulation to finished retail carton.
Our state-of-the-art facility in Selma, Texas features climate-controlled staging zones, positive-pressure air handling, and HEPA-filtered cleanroom filling suites to eliminate environmental contaminants.
Operating dual automated production shifts, our lines process over 5 million finished units daily, providing the scalabilities required to handle massive seasonal spikes without lead-time delays.
Our plant operates under strict FDA cGMP registration, NSF certifications, Informed Choice sport testing compliance, and CE machinery directives for seamless European export validation.
Key operational, regulatory, and technical insights for sourcing managers, brand founders, and international procurement teams.
Partner with a trusted U.S. contract manufacturer and exporter. Contact our technical engineering team today to review your formulation specs, bottle requirements, target delivery timelines, and bulk tier pricing.